

1. Introduction – Batch Packing Record for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel:
The Batch Packing Record (BPR) for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel provides documented instructions and controls for the filling, sealing, coding, packing, inspection, reconciliation, and release of the finished gel product. The document identifies the product as IGMADINE 20 GM and specifies the formulation containing Diclofenac Diethylamine equivalent to Diclofenac Sodium 1% w/w, Linseed Oil 3.00% w/w, Methyl Salicylate 10.00% w/w, Menthol 5.00% w/w, and Benzyl Alcohol 1.00% w/w. It also specifies storage at a temperature not exceeding 25°C and protection from freezing. The BPR establishes systematic controls for packing material dispensing, overprinting, line clearance, tube filling and sealing, carton and shipper packing, in-process checks, defect or deviation recording, sample collection, and final verification. Before filling and packing activities begin, the document requires verification of area and equipment cleanliness, environmental conditions, change parts, dispensed packing materials, coding arrangements, and calibration status of the weighing balance, followed by QA line clearance. During tube filling, the BPR requires monitoring of the target weight of 30.9 g, an acceptable filling range of 30.0–32.7 g, cap-sealing status, and periodic checks at a frequency of 60 minutes. Overall, this BPR supports GMP compliance, traceability, packing accuracy, prevention of mix-ups, in-process control, reconciliation, and documented batch release for the gel product.
Skip to PDF content2. Flow Diagram – Batch Packing Record for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel:
The Batch Packing Record for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel describes the controlled sequence of activities required for filling, sealing, coding, packing, inspection, reconciliation, and final release of the finished gel product. The product is identified as IGMADINE 20 GM, containing Diclofenac Diethylamine equivalent to Diclofenac Sodium 1% w/w, Linseed Oil 3.00% w/w, Methyl Salicylate 10.00% w/w, Menthol 5.00% w/w, and Benzyl Alcohol 1.00% w/w. The process begins with verification of area and machine cleanliness, removal of previous product or packing materials, readiness of change parts, availability of approved packing materials, and QA line clearance before starting filling and packing operations. Packing materials such as laminated tubes, inner cartons, multicartons, shippers, and BOPP tape are dispensed and recorded before use.
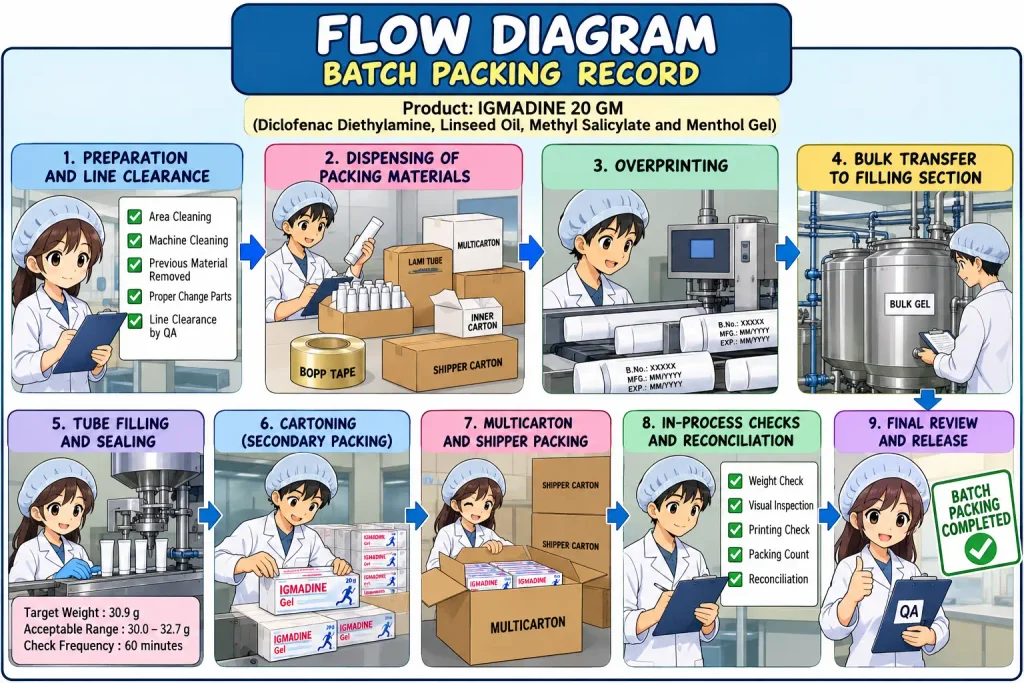
Overprinting activities are checked to ensure correct batch number, manufacturing date, expiry date, MRP, and other required coding details. During tube filling, the gel is filled into approved tubes, capped, sealed, and subjected to in-process weight verification. The target weight is 30.9 g, with an acceptable filling range of 30.0–32.7 g, and checks are performed at a frequency of 60 minutes. After filling, tubes are packed into cartons, multicartons, and shippers. Coding, shipper contents, packing accuracy, rejection quantities, sample collection, reconciliation, deviations, and final QA verification are documented to ensure complete traceability, GMP compliance, and controlled batch release.
3. Critical Process Parameters (CPP) and Critical Quality Attributes (CQA) for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel:
The Critical Process Parameters (CPP) and Critical Quality Attributes (CQA) for Diclofenac Diethylamine, Linseed Oil, Methyl Salicylate and Menthol Gel are important controls used to ensure consistent packing performance and acceptable finished-product quality. The batch packing record identifies the product as IGMADINE 20 GM and lists Diclofenac Diethylamine equivalent to Diclofenac Sodium 1% w/w, Linseed Oil 3.00% w/w, Methyl Salicylate 10.00% w/w, Menthol 5.00% w/w, and Benzyl Alcohol 1.00% w/w.
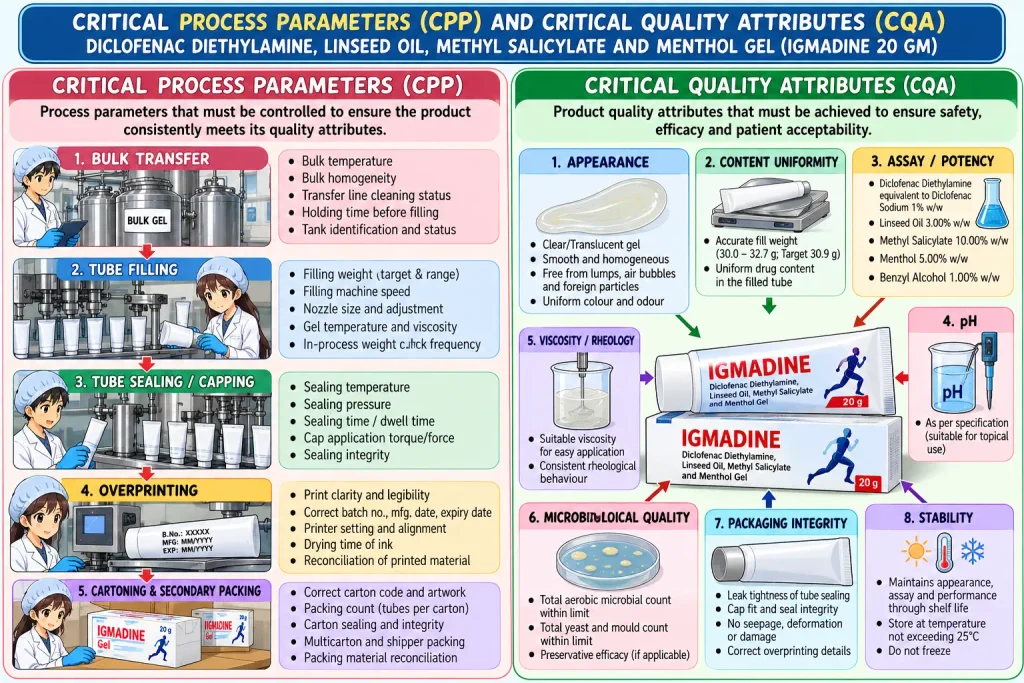
For packing operations, important process controls include correct line clearance, verification of cleaned equipment and change parts, approved packing materials, correct coding and overprinting details, tube filling, cap closing, sealing, and periodic weight checks. The BPR specifies a target filled weight of 30.9 g, an acceptable filling range of 30.0–32.7 g, and an in-process checking frequency of 60 minutes.Proper control of these parameters helps prevent underfilling, overfilling, sealing defects, coding errors, and packaging mix-ups.From the packing-record perspective, key quality attributes include correct fill quantity, acceptable tube sealing, accurate batch and date coding, correct carton and shipper contents, proper packaging identification, and acceptable finished-pack integrity. The record also requires monitoring of recoverable and non-recoverable rejections, carton and shipper packing checks, defect or deviation documentation, sampling, reconciliation, and final QA verification.Together, CPP and CQA controls support product consistency, packaging integrity, traceability, GMP compliance, prevention of mix-ups, and reliable batch release throughout the packing process.